
Iron Phosphate Pretreatment
For Powder Coating
Iron phosphate pretreatment cleans steel and leaves a phosphate conversion coating that helps powder and paint adhere. CPR Systems has made single-step phosphate chemistry since 1989 (PhosBite 101) and pairs it with spray wand or stage washer equipment that recycles the wash water to zero discharge.
Proven Since 1989
PhosBite 101 single-step phosphate chemistry, made by CPR since 1989.
Single Step
Clean And Coat
Efficient clean and coat operations hot water wash operation for quick wash to dry.
Zero Discharge
EPA Compliance
Over 80% reduction in water and chemical consumption. Nothing is sent to drain.
Paint Adhesion
Corrosion Resistance
Conversion coatings for increased paint adhesion. RO rinse and seal coat compatible.

CPR Systems
BondTite Washer
MDL-20 Filtration Platform
Single Step Clean And Phosphate
Zero Discharge, Closed Loop Recycling
Runs In Spray Wand And Stage Washer Systems
It is a cleaner-degreaser that also deposits a thin iron phosphate coating on ferrous metal in the same step. The coating improves adhesion and slows under-film corrosion.
How Does The Spray Phosphating Process Work?
-
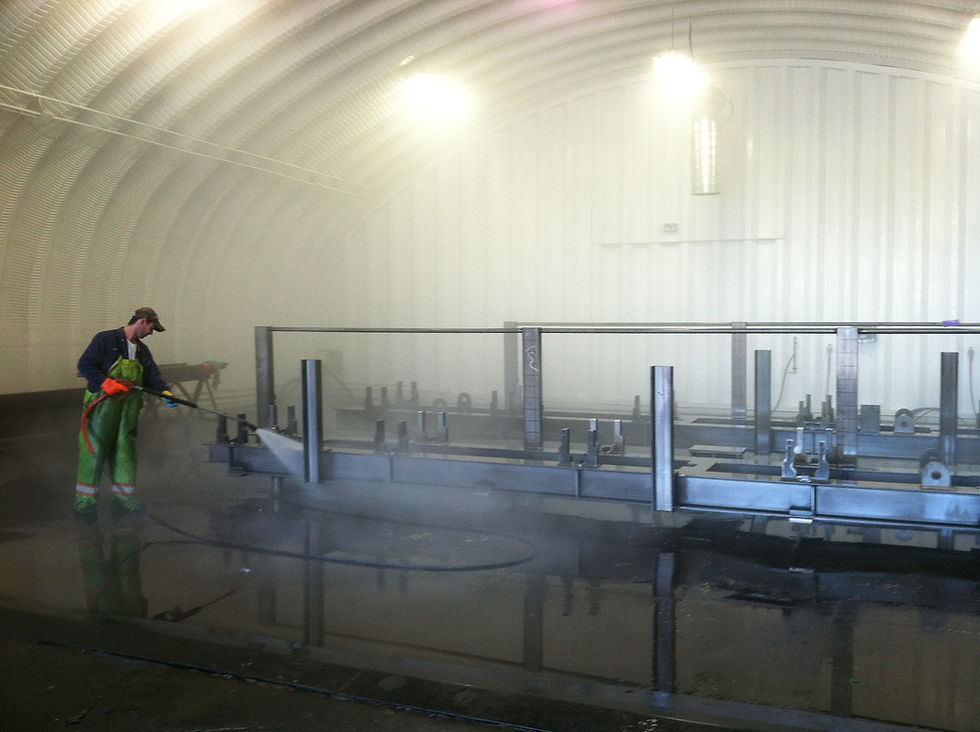
Hot-water spray, with pressures up to 3,000 PSI and temps up to 180 degrees, cleans and phosphates in one pass.
-
No rinse required: the system is built to run as a non-rinse process when the chemistry is titrated and operated properly. If you choose to rinse, city, well or RO water all work. Optional seal coat.
-
Dry-off, then powder coat or paint.
-
Wash water filtered to 20 microns and reused; nothing goes to drain.
Which Phosphate Chemistry Fits Your Parts?
PhosBite 101 (steel): standard steel parts; proven since 1989.
PhosBite M+ (steel and aluminum): mixed-metal lines, with a fluoride additive.
PhosBite M4000 (steel and aluminum): bare metal parts with heavier oil saturation; double the cleaner of M+.
Seal coat (optional): added corrosion protection after phosphate.
Should You Use Phosphate Or Zirconium?
Iron phosphate is a proven choice for steel, and drum pricing for the two is close. Zirconium suits mixed steel and aluminum and removes phosphate from the waste stream. See zirconium pretreatment.
Comparing options? See how to choose a metal pretreatment system.
Not Sure About Your Coating Weights?
Not sure your current phosphate is giving you good coating weights? We'll test panels with your parts for free. Call 574-233-9111 or request a free panel test below.
Installation, Training, After Care
Our pretreatment packages include installation of equipment, training at your facility and after start-up remote support via our online maintenance tracking programs.


Iron Phosphate Pretreatment FAQ
Can I use iron phosphate before powder coating?
Yes; it is the most common pretreatment for steel before powder coating.
What coating weight should iron phosphate produce?
It depends on the chemistry you use, the concentration you run and how it's applied. If you're working to a customer spec or finishing protocol, tell us what it is and we'll work backward to the chemistry and setup that meets it. A free panel test on your parts confirms the result in your process.
Can I phosphate with a pressure washer?
Yes, with a heated, chemical-rated system such as CPR's spray wand pretreatment.
How do I get rid of phosphate wastewater?
CPR filtration recycles it so it isn't discharged. See wash water recycling.
What is a rinse and seal after iron phosphate?
After the phosphate wash, parts get a clean-water rinse to remove leftover chemistry, then a seal coat that adds corrosion protection before powder. CPR lines run the rinse with city, well or RO water and add the seal as an option. Caterpillar's High Performance B level uses an RO rinse and seal; Standard Performance C uses a tap-water rinse.
Do I need a seal after iron phosphate?
It depends on the spec on your drawing or PO. Tell us the spec and we'll work backward to the stages you need, and we clean sample panels free so you can run your own tests.
